Category: Advanced

SIPOC Explained: How to Define Processes and Drive Lean Six Sigma Success-Part-2

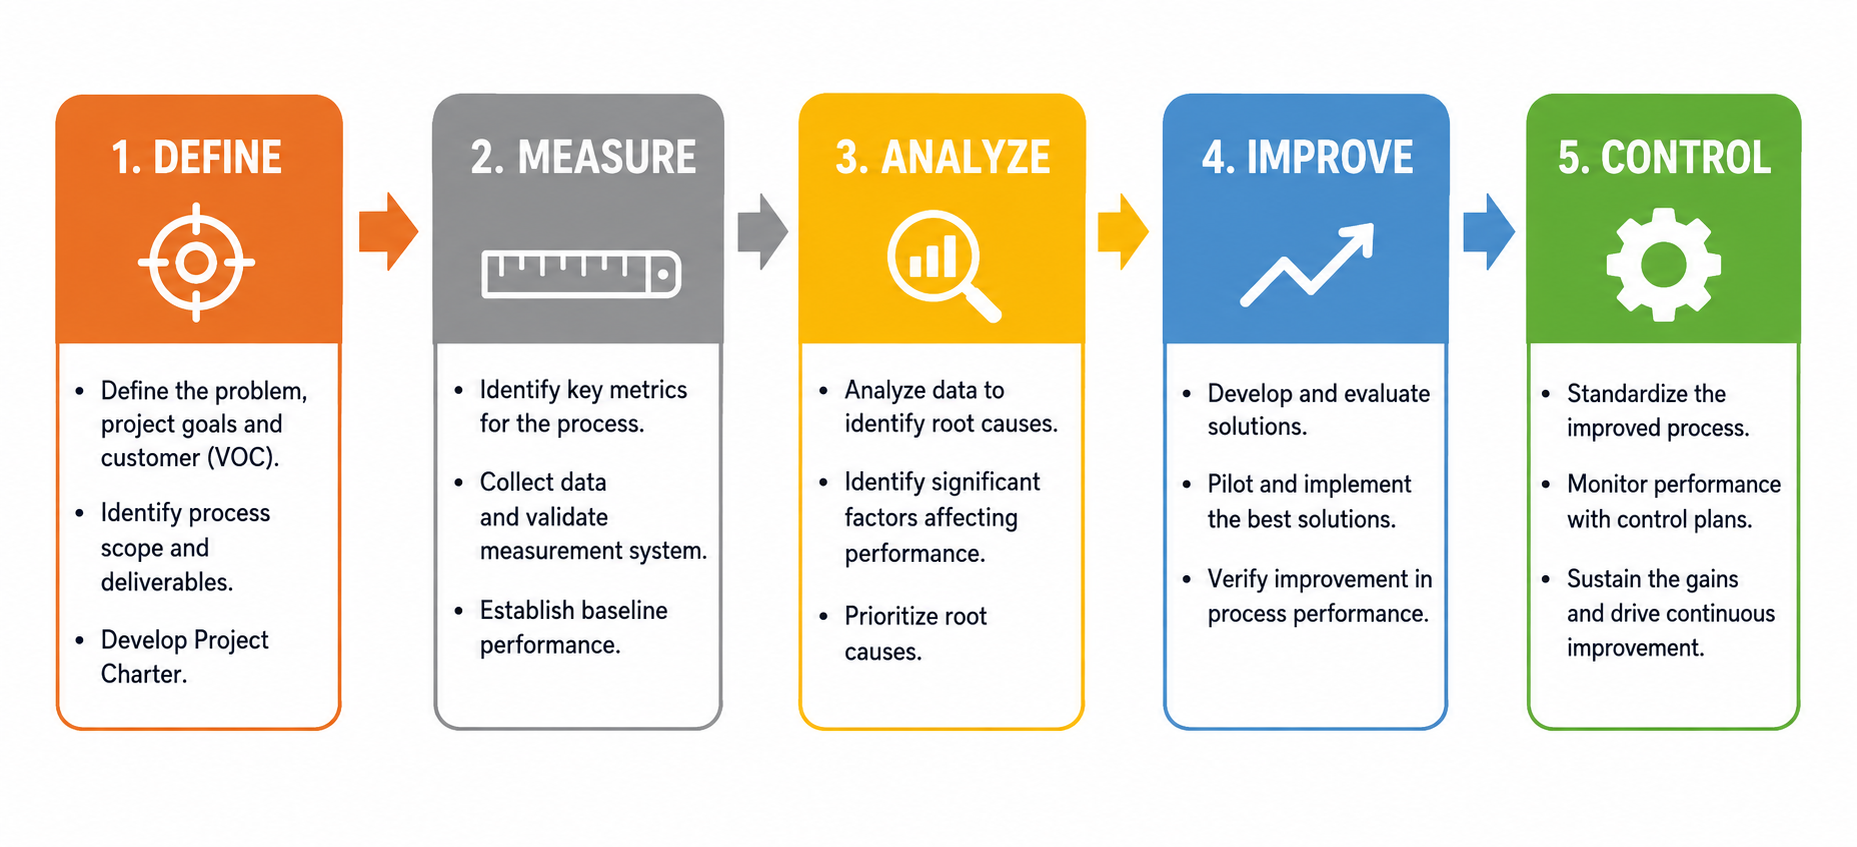
H2: SIPOC vs Value Stream Mapping SIPOC and Value Stream Mapping serve different purposes: SIPOC is often the starting point, while VSM provides deeper insights. H2: Why SIPOC Is Still Relevant Today SIPOC is widely used across industries, including: Manufacturing IT and services Healthcare Finance Digital transformation Its simplicity makes it adaptable, while its structure makes it powerful. H2: Conclusion: Start with Clarity, Then Improve Many organizations focus on tools, data, and technology. However, true improvement begins with clarity. SIPOC provides that clarity by: Defining process boundaries Aligning stakeholders Identifying dependencies Establishing a strong foundation Before analyzing or improving any process, take the time to understand it. Because when the process is clearly defined, improvement becomes prec.ise and effective Internal Linking Suggestions Lean Six Sigma Training page DMAIC methodology blog Value Stream Mapping blog Example: Tools like value stream mapping can be used after SIPOC to analyze process flow in detail. SEO Checklist (Elementor Ready) ✔ Primary keyword used (SIPOC in Lean Six Sigma) ✔ H1, H2, H3 structured ✔ Short paragraphs ✔ Image placements with ALT text ✔ Internal linking opportunities ✔ Meta title + description included SIPOC in Lean Six Sigma: The Ultimate Guide to Process Definition and Clarity In every improvement journey, clarity must come before action. Organizations often rush into data collection, root cause analysis, or solution design without first asking a critical question: What exactly is the process we are trying to improve? This lack of clarity is one of the most common reasons why improvement projects fail. Teams argue about scope. Stakeholders disagree on boundaries. Data is collected on the wrong areas. Solutions are implemented without alignment. Lean Six Sigma addresses this risk through a deceptively simple yet extraordinarily powerful tool called the SIPOC diagram. SIPOC is a high-level process mapping tool used to define and frame a process before improvement begins. Though simple in appearance, SIPOC has the power to align cross-functional teams, clarify scope, and prevent costly project misdirection. This article provides a comprehensive guide to understanding SIPOC, its strategic importance, how to create one correctly, common mistakes to avoid, real-world applications, and how organizations can leverage it for sustainable improvement. What Is a SIPOC Diagram? SIPOC is an acronym that stands for Suppliers, Inputs, Process, Outputs, and Customers. It represents a structured view of a process from beginning to end, capturing its essential elements on a single page. Unlike detailed process maps, SIPOC does not attempt to document every step. Instead, it provides a high-level snapshot of how value flows through a system. It defines the boundaries of the process, identifies who provides inputs, outlines the core process steps, describes the outputs produced, and clarifies who receives those outputs. The true power of SIPOC lies not in its complexity but in its ability to bring alignment. When a cross-functional team creates a SIPOC diagram together, hidden assumptions surface. Differences in understanding become visible. Boundaries become clear. Before measuring or improving anything, teams must agree on what they are working on. SIPOC ensures that agreement. Why SIPOC Is Critical in Lean Six Sigma Projects In the DMAIC methodology, the Define phase sets the direction for the entire project. If the Define phase lacks clarity, every subsequent phase suffers. SIPOC plays a foundational role in this stage because it establishes process scope and alignment before data collection begins. Without SIPOC, teams often fall into one of three traps. They define the scope too broadly and become overwhelmed. They define it too narrowly and miss systemic causes. Or they fail to align stakeholders, resulting in resistance later in the project. SIPOC forces structured thinking. It requires the team to articulate exactly where the process starts and ends. It clarifies who is upstream and who is downstream. It prevents scope creep and ensures improvement efforts are targeted and strategic. In many ways, SIPOC is not just a process mapping tool. It is a risk mitigation tool. Breaking Down the Five Components of SIPOC Understanding SIPOC requires deeper exploration of its five elements. Suppliers Suppliers are the entities that provide inputs to the process. They may be internal departments, external vendors, systems, or even regulatory bodies. A supplier is not limited to physical goods. Information providers, data systems, and service teams can all be suppliers. Identifying suppliers clarifies dependencies. It highlights where variation may originate. In many cases, problems attributed to internal processes actually stem from inconsistent inputs supplied upstream. Recognizing suppliers early in a project ensures that improvement efforts do not ignore upstream influences. Inputs Inputs are the materials, information, requests, or triggers that initiate and sustain the process. Inputs are consumed, transformed, or used within the process. For example, in a customer onboarding process, inputs may include application forms, identification documents, or customer data. In manufacturing, inputs may include raw materials, machine settings, and specifications. Clarity around inputs helps teams define measurable parameters. It also highlights the importance of input quality. Poor outputs often originate from unstable inputs. Process The process section of SIPOC includes high-level steps, typically limited to five to seven stages. The goal is not detail but structure. For instance, a recruitment process might be summarized as sourcing candidates, screening resumes, conducting interviews, making offers, and onboarding. Each of these stages could later be expanded into detailed process maps, but at the SIPOC stage, brevity ensures clarity. Limiting the number of process steps prevents teams from prematurely diving into operational minutiae. Outputs Outputs are the products, services, or deliverables generated by the process. Outputs may be tangible or intangible. They must be clearly defined and measurable. Outputs often serve as inputs to another process. Recognizing this interconnectedness encourages systems thinking. When outputs are poorly defined, customer expectations remain ambiguous. SIPOC helps define outputs precisely, creating a foundation for quality measurement. Customers Customers are the recipients of the outputs. They may be external clients, internal departments, or downstream processes. Identifying customers is critical because improvement efforts must ultimately enhance customer value. Without clarity on who the customer is, teams risk optimizing internal efficiency without improving outcomes. Customer

Explore More
SIPOC Explained: How to Define Processes and Drive Lean Six Sigma Success-Part-1

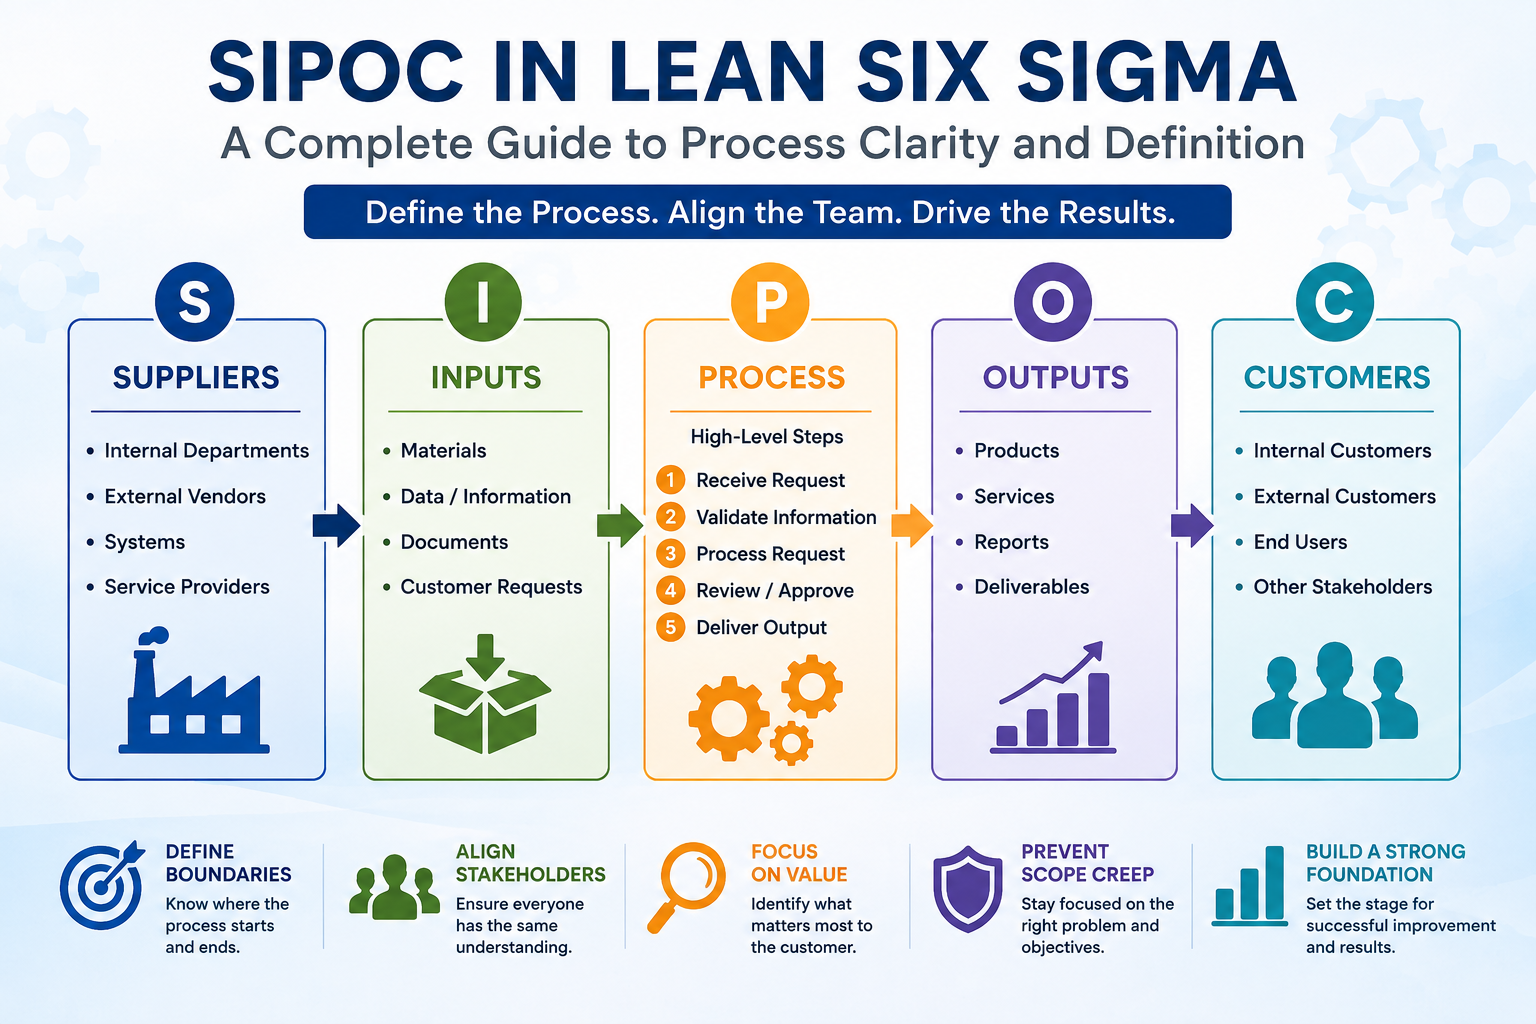
H1: SIPOC in Lean Six Sigma: A Complete Guide to Process Clarity and Definition Meta Title SIPOC in Lean Six Sigma: A Complete Guide to Process Mapping and Clarity Meta Description Learn how SIPOC helps define processes, align teams, and improve project success in Lean Six Sigma. A practical guide with examples and steps. Introduction Every successful improvement initiative begins with one critical step—understanding the process clearly. However, in many organizations, teams rush into data analysis, root cause identification, or solution implementation without first defining what exactly needs improvement. This often leads to confusion, misalignment, and ineffective results. Projects fail not because of poor tools, but because of unclear process boundaries and lack of alignment. This is where the SIPOC diagram becomes essential. SIPOC is one of the most powerful yet simple tools in Lean Six Sigma. It helps teams define the process at a high level, align stakeholders, and ensure everyone is working toward the same objective. In this blog, we will explore: What SIPOC is Why it is critical in Lean Six Sigma How to create it step by step Common mistakes to avoid Real-world applications H2: What Is a SIPOC Diagram? SIPOC stands for: Suppliers Inputs Process Outputs Customers It is a high-level process mapping tool that provides a complete overview of how a process works. Unlike detailed flowcharts, SIPOC focuses on clarity rather than complexity. It captures the essential elements of a process on a single page. It helps answer key questions: Where does the process start and end? What inputs are required? What outputs are generated? Who are the customers? The real strength of SIPOC lies in alignment. When teams create a SIPOC together, differences in understanding become visible, and clarity emerges. Image Suggestion (Place here) SIPOC diagram showing Suppliers → Inputs → Process → Outputs → Customers Alt Text: SIPOC diagram for process mapping in Lean Six Sigma H2: Why SIPOC Is Critical in Lean Six Sigma Projects In the DMAIC methodology, the Define phase sets the foundation for the entire project. If this phase is weak, the entire project suffers. SIPOC plays a key role here by: Defining process boundaries Aligning stakeholders Preventing scope creep Ensuring focus on the right problem Without SIPOC, teams often face: Confusion about scope Misaligned expectations Incorrect data collection Ineffective solutions SIPOC acts as a risk prevention tool, ensuring that improvement efforts start on the right path. H2: Why SIPOC Is Critical in Lean Six Sigma Projects In the DMAIC methodology, the Define phase sets the foundation for the entire project. If this phase is weak, the entire project suffers. SIPOC plays a key role here by: Defining process boundaries Aligning stakeholders Preventing scope creep Ensuring focus on the right problem Without SIPOC, teams often face: Confusion about scope Misaligned expectations Incorrect data collection Ineffective solutions SIPOC acts as a risk prevention tool, ensuring that improvement efforts start on the right path. H2: Understanding the Five Elements of SIPOC To use SIPOC effectively, it is important to understand each component clearly. H3: Suppliers Suppliers are the sources that provide inputs to the process. They can include: Internal departments External vendors Systems or databases Service providers Identifying suppliers helps uncover upstream dependencies that may impact process performance. H3: Inputs Inputs are the resources required for the process to function. These may include: Raw materials Data or information Customer requests Documents Poor-quality inputs often lead to poor outputs, making this step critical. H3: Process This section defines the high-level steps involved in the process. Typically, it includes 5–7 major steps to maintain clarity. For example: Receive request Validate information Process request Deliver output The focus is on structure, not detailed steps. H3: Outputs Outputs are the results produced by the process. They can be: Products Services Reports Deliverables Clearly defining outputs ensures measurable results. H3: Customers Customers are the recipients of the outputs. They can be: External clients Internal teams End users Understanding customers ensures that the process delivers value, not just efficiency. H2: How to Create a SIPOC Diagram (Step-by-Step) Creating a SIPOC diagram should be a collaborative activity involving cross-functional teams. Follow these steps: Step 1: Define Process Boundaries Clearly identify where the process starts and ends. Without clear boundaries, the process becomes difficult to manage. Step 2: Identify High-Level Process Steps List 5–7 key steps that define the process. Avoid going into too much detail at this stage. Step 3: Define Outputs Ask: What does this process produce? Who receives it? This helps clarify value delivery. Step 4: Identify Customers Determine who benefits from the outputs. This ensures customer-focused improvement. Step 5: Identify Inputs List the resources required to execute the process. Step 6: Identify Suppliers Finally, identify who provides the inputs. 💡 Tip: Although SIPOC reads left to right, it is often easier to build it starting from the Process column. Image Suggestion (Place here) Flowchart showing SIPOC creation steps Alt Text: Steps to create a SIPOC diagram in Lean Six Sigma H2: Real-World Example – SIPOC for Pizza Manufacturing Let’s consider a simple example. Suppliers Ingredient vendors (flour, cheese, vegetables) Inputs Raw materials, recipes, order details Process Preparation → Assembly → Baking → Inspection → Packaging Outputs Ready-to-deliver pizza Customers End customers or retail outlets This example highlights how SIPOC provides a clear and structured overview of the process. Image Suggestion (Place here) SIPOC diagram for pizza manufacturing process Alt Text: SIPOC example for manufacturing process H2: Common Mistakes in SIPOC Creation Despite its simplicity, SIPOC is often misused. Adding Too Much Detail SIPOC is a high-level tool, not a detailed process map. Poorly Defined Boundaries Unclear start and end points lead to confusion. Lack of Stakeholder Involvement Creating SIPOC in isolation results in incomplete understanding. Treating It as a Formality SIPOC should be used for alignment, not just documentation. H2: Strategic Benefits of SIPOC SIPOC offers several organizational benefits: Improves cross-functional communication Clarifies roles and responsibilities Identifies dependencies Enables better decision-making Builds a structured improvement culture For leadership, SIPOC provides a simple view of

Explore More

Lean Thinking in the Gas Distribution Industry: Driving Safety, Reliability, and Operational Excellence-Part-2

Lean Principles Applied to Gas Distribution Lean thinking is built around five core principles that guide improvement initiatives. Identify Customer Value The first step is understanding what customers truly value. In gas distribution, customers expect: Reliable gas supply Safe operations Fast service response Transparent billing Any activity that does not contribute to these outcomes should be examined carefully. Map the Value Stream Value Stream Mapping involves visualizing the entire process from supply to customer delivery. This exercise helps organizations identify bottlenecks, delays, and unnecessary steps. For example, mapping the cylinder distribution process may reveal multiple approvals or documentation steps that slow down delivery operations. Create Flow Once waste is identified, processes should be redesigned to create smooth operational flow. This may involve reorganizing workstations, simplifying procedures, or improving coordination between departments. Establish Pull Systems Lean encourages demand-driven operations rather than producing output in anticipation of demand.In gas utilities, this principle can help optimize inventory management and avoid overproduction. Pursue Continuous Improvement Lean is not a one-time initiative but a continuous improvement journey. Organizations must constantly monitor processes and seek opportunities for incremental improvements. Lean Opportunities in Gas Distribution Operations Lean thinking can unlock significant improvement opportunities across various operational areas. Lean Tools for Gas Utilities Several practical Lean tools can support improvement initiatives. Benefits of Lean in the Gas Industry Organizations that adopt Lean thinking can achieve substantial benefits. Operational Benefits Improved asset utilization Faster service delivery Reduced operational delays Financial Benefits Lower operating costs Reduced inventory carrying costs Improved resource utilization Safety Benefits Lean processes reduce operational complexity, which contributes to safer operations. Customer Benefits Customers benefit from faster service, improved reliability, and consistent service quality. Building a Lean Culture in Gas Organizations Sustainable improvement requires more than tools—it requires culture. Lean organizations encourage employees at all levels to participate in improvement initiatives. Key elements of a Lean culture include: Leadership commitment Employee engagement Continuous learning Data-driven decision making Training programs play an important role in building this capability across the organization. How ICEQBS Supports Lean Transformation ICEQBS helps organizations implement structured process improvement programs that drive measurable results. Through training, consulting, and hands-on improvement projects, ICEQBS supports organizations in: diagnosing operational inefficiencies redesigning business processes building internal improvement capability sustaining continuous improvement programs By combining practical expertise with industry best practices, ICEQBS helps organizations transform operations and achieve long-term performance excellence. Conclusion The gas distribution industry operates in an environment where reliability, safety, and efficiency are paramount. As operational complexity continues to increase, organizations must adopt structured improvement approacwhes to remain competitive and resilient. Lean thinking offers a powerful framework for identifying inefficiencies, eliminating waste, and improving operational flow. By focusing on value creation and continuous improvement, gas utilities can enhance both operational performance and customer satisfaction. For organizations seeking to strengthen operational excellence, Lean is not simply a methodology—it is a strategic capability that drives long-term success.  

Explore More

Lean Thinking in the Gas Distribution Industry: Driving Safety, Reliability, and Operational Excellence-Part-1

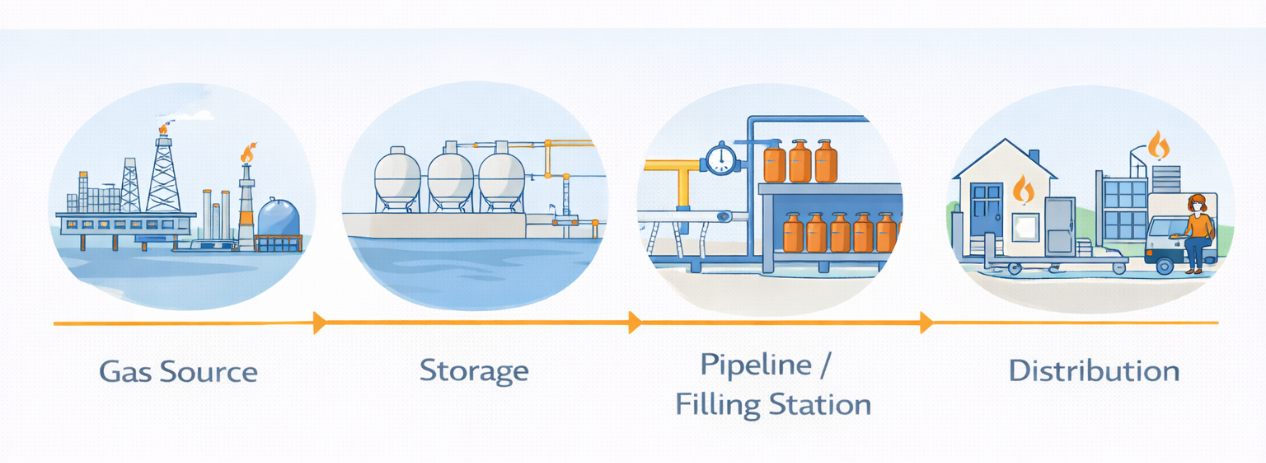
Introduction: Why Lean Thinking Matters in the Gas Industry The gas distribution industry plays a vital role in modern economies. From residential cooking fuel to industrial energy supply, gas utilities form part of the critical infrastructure that powers homes, businesses, and industries. Reliability, safety, and operational efficiency are therefore not optional—they are essential. However, gas distribution operations are inherently complex. Organizations must manage pipelines, storage facilities, filling stations, delivery logistics, safety monitoring systems, and customer service operations. Each of these processes involves numerous handoffs, regulatory requirements, and operational risks. In such environments, even small inefficiencies can cascade into major operational challenges. Delays in cylinder filling operations can affect delivery schedules. Inefficient maintenance practices can increase equipment downtime. Poor inventory management can lead to stock shortages or excess holding costs. Many of these issues stem from hidden inefficiencies embedded in everyday operations. Teams may spend time waiting for approvals, searching for tools, handling rework, or managing unnecessary paperwork. Over time, these inefficiencies accumulate and significantly affect productivity, cost structures, and service reliability. This is where Lean thinking becomes particularly powerful. Lean is a management philosophy focused on maximizing customer value while minimizing waste. Originating from the Toyota Production System, Lean has evolved into a globally recognized approach for improving operational efficiency across industries—including manufacturing, healthcare, logistics, and energy utilities. For gas distribution companies, Lean offers a structured way to streamline operations, eliminate inefficiencies, and build a culture of continuous improvement. By focusing on value creation and waste elimination, organizations can enhance operational reliability while maintaining the highest standards of safety and compliance. Understanding the Gas Distribution Ecosystem Gas distribution is a multi-layered operational system that requires careful coordination between infrastructure, workforce, technology, and regulatory oversight. At a high level, the gas distribution value chain includes the following stages: Supply and Storage Gas is sourced from upstream suppliers and stored in dedicated facilities before being transported through distribution networks. Transportation and Pipeline Networks Gas travels through an extensive network of pipelines, regulators, and monitoring systems that ensure safe and efficient flow. Cylinder Filling and Bottling Operations For LPG-based systems, gas is transferred into cylinders at specialized filling plants before being distributed to customers. Logistics and Distribution Cylinder distribution involves route planning, vehicle management, and coordination with local distributors. Customer Connections and Service Gas companies handle new customer connections, service requests, billing inquiries, and complaint resolution. Maintenance and Safety Monitoring Continuous inspection and maintenance ensure pipeline integrity, equipment reliability, and regulatory compliance. Each of these stages involves numerous operational processes. When these processes are not streamlined, inefficiencies can quickly emerge. For example: Field technicians may travel long distances due to poor route planning. Maintenance teams may spend excessive time locating spare parts. Cylinder filling operations may experience bottlenecks during peak demand periods. Such inefficiencies not only increase operating costs but can also affect service reliability and customer satisfaction. Lean thinking helps organizations address these challenges by examining the entire operational system and identifying opportunities for improvement. Operational Challenges in Gas Utilities Gas distribution organizations face a unique set of operational challenges that require careful management. Infrastructure Complexity Gas utilities operate large networks of pipelines, compressors, valves, regulators, and storage facilities. Maintaining these assets requires careful planning and coordination. Unexpected equipment failures can disrupt supply and create safety risks. Field Service Coordination Technicians are responsible for inspections, maintenance, repairs, and emergency response activities. Inefficient dispatching systems or unclear procedures can lead to delays in service delivery. Maintenance and Asset Management Many organizations rely on reactive maintenance practices where equipment is repaired only after failure occurs. This approach increases downtime and operational risk. Customer Service Expectations Customers expect reliable gas supply and timely service. Delays in connection requests or complaint resolution can negatively affect customer satisfaction. Inventory Management Spare parts, cylinders, and maintenance equipment must be carefully managed. Excess inventory ties up capital, while shortages can delay maintenance activities. Regulatory Compliance Gas utilities operate under strict regulatory frameworks that require detailed documentation, safety inspections, and compliance reporting. These operational challenges often create layers of complexity within organizations. Without structured improvement approaches, inefficiencies remain hidden within everyday processes. Lean thinking provides a framework for identifying and removing these inefficiencies. Introduction to Lean Thinking Lean thinking focuses on one central idea: creating maximum value for customers while eliminating activities that do not add value. In Lean terminology, non-value activities are called waste. Waste refers to any activity that consumes resources without contributing to customer value. In many organizations, a significant portion of daily work consists of such non-value activities. Lean identifies eight common types of waste: In gas distribution operations, these wastes may appear in various forms: Waiting time during cylinder filling operations Excess spare parts inventory in maintenance warehouses Repeated paperwork during safety inspections Long travel distances for field technicians By systematically identifying and eliminating these wastes, organizations can significantly improve operational efficiency.

Explore More

Stop Treating Symptoms. Fix the Cause: Mastering Y = f(x) the Six Sigma Way

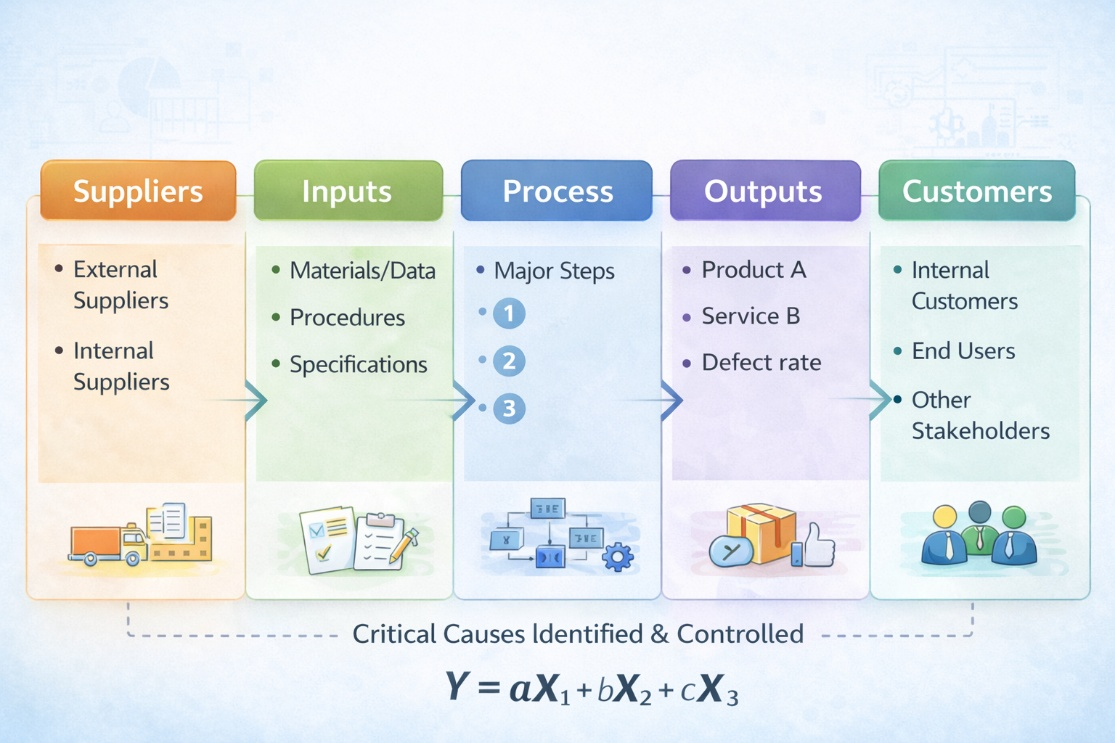
Introduction: Why Problems Keep Coming Back (Even After “Fixes”) Every organization wants better outcomes—fewer defects, faster delivery, happier customers, and predictable performance. Yet when results start slipping, most teams go into firefighting mode. More reviews. More pressure. More follow-ups. More “urgent” calls. For a short time, things improve. Then the same problems return. This cycle repeats because teams try to fix the result instead of fixing what caused the result. In Six Sigma, this misunderstanding is addressed by a simple but powerful idea: Y = f(x) Your results (Y) are a function of your causes (X). Once teams internalize this, problem-solving changes from reactive to systematic—and improvements begin to sustain. In any process, Y represents the outcome you want to improve: Defect rate Turnaround time Customer complaints SLA breaches Sales conversion Rework percentage These are called output variables or dependent variables—they depend on what happens inside the process. X represents the inputs and conditions that shape those outcomes: People (skills, training, fatigue, adherence to SOPs) Machines (settings, calibration, downtime) Methods (handoffs, approvals, rework loops) Materials/Data (quality, completeness) Measurement (definitions, inspection methods) Environment (workload, system uptime, distractions) These are independent variables. When X changes, Y changes. When X is unstable, Y becomes unstable. The core message: You can’t command results to improve. You can only improve the process conditions that create those results. Why Fixing Only the Output Never Works When defects rise, common reactions include: Pushing people harder Adding more checks Escalating to managers Extending working hours These actions may temporarily improve numbers. But they don’t remove the reason the problem occurred. Results are produced by the process. You can’t sustainably change results without changing the process conditions. This is the mindset shift Y = f(x) creates: From “who failed?” to “which variable changed?” This reduces blame, increases clarity, and builds ownership of the process. A Simple Real-Life Analogy (Why Treating the Wrong Cause Fails) Think of a headache. The headache is Y (the effect). Possible causes (X) include lack of sleep, dehydration, eye strain, stress, or infection. If dehydration is the cause and you take a stress tablet, the headache persists. Organizations do the same: Complaints rise → send warning emails Delays increase → push overtime Defects rise → scold operators If the real cause is poor machine calibration or unclear SOPs, none of these actions will fix the problem. Six Sigma teaches teams to validate causes with data before acting. Applying Y = f(x) to a Real Business Problem (Step-by-Step) Imagine a defect rate of 8% with a target of 4%. Step 1: Identify Possible Causes Teams brainstorm broadly: machine settings, training gaps, material quality, shift differences, workload spikes, unclear SOPs. This may yield 30–50 possible X’s. Step 2: Prioritize Likely Causes Using process maps and Cause & Effect Matrices, narrow down to 10–15 likely contributors. This focuses effort. Step 3: Validate the Critical X’s with Data Collect data for shortlisted X’s. Use Pareto, correlation, regression, or hypothesis testing to identify the 3–5 critical X’s that truly drive defects. This often yields a practical relationship like: Y = aX₁ + bX₂ + cX₃ Step 4: Improve Only What Matters Design solutions that directly target the critical X’s. Avoid spreading effort across low-impact factors. Step 5: Control the X’s to Sustain Results Set controls for critical X’s (standard work, control charts, audits). When X remains stable, Y remains stable. Tools That Help You Find and Control the Critical X’s Process Mapping:See where X’s enter the process Fishbone (Cause & Effect):Structure hypotheses Pareto Analysis:Focus on the vital few X’s Regression/Correlation:Quantify relationships DOE (Design of Experiments):Test cause-effect rigorously Control Charts:Keep critical X’s stable over time These tools turn Y = f(x) from theory into action. The Cultural Shift Y = f(x) Creates Before Y = f(x), teams ask: Why are people not performing? Why are targets not met? After Y = f(x), teams ask: Which process variable changed? Which input went out of control? Which root cause is driving this result? This shift reduces blame, improves clarity, and creates predictable performance. Common Pitfalls (Why Teams Struggle to Apply Y = f(x)) Jumping to solutions without validating causes Treating all causes as equal (not prioritizing critical X’s) Collecting data without clear definitions Failing to control X’s after improvement Treating Y = f(x) as a slogan, not a method Avoiding these pitfalls is what separates short-term wins from sustained improvement. Final Takeaway: Control the Cause, and the Result Takes Care of Itself If the same problems keep returning, the issue isn’t effort—it’s focus. When teams focus on the result, problems resurface. When teams control the right causes, results stabilize naturally.

Explore More

Data Types in Six Sigma: How Choosing the Right Data Transforms Your Improvement Results

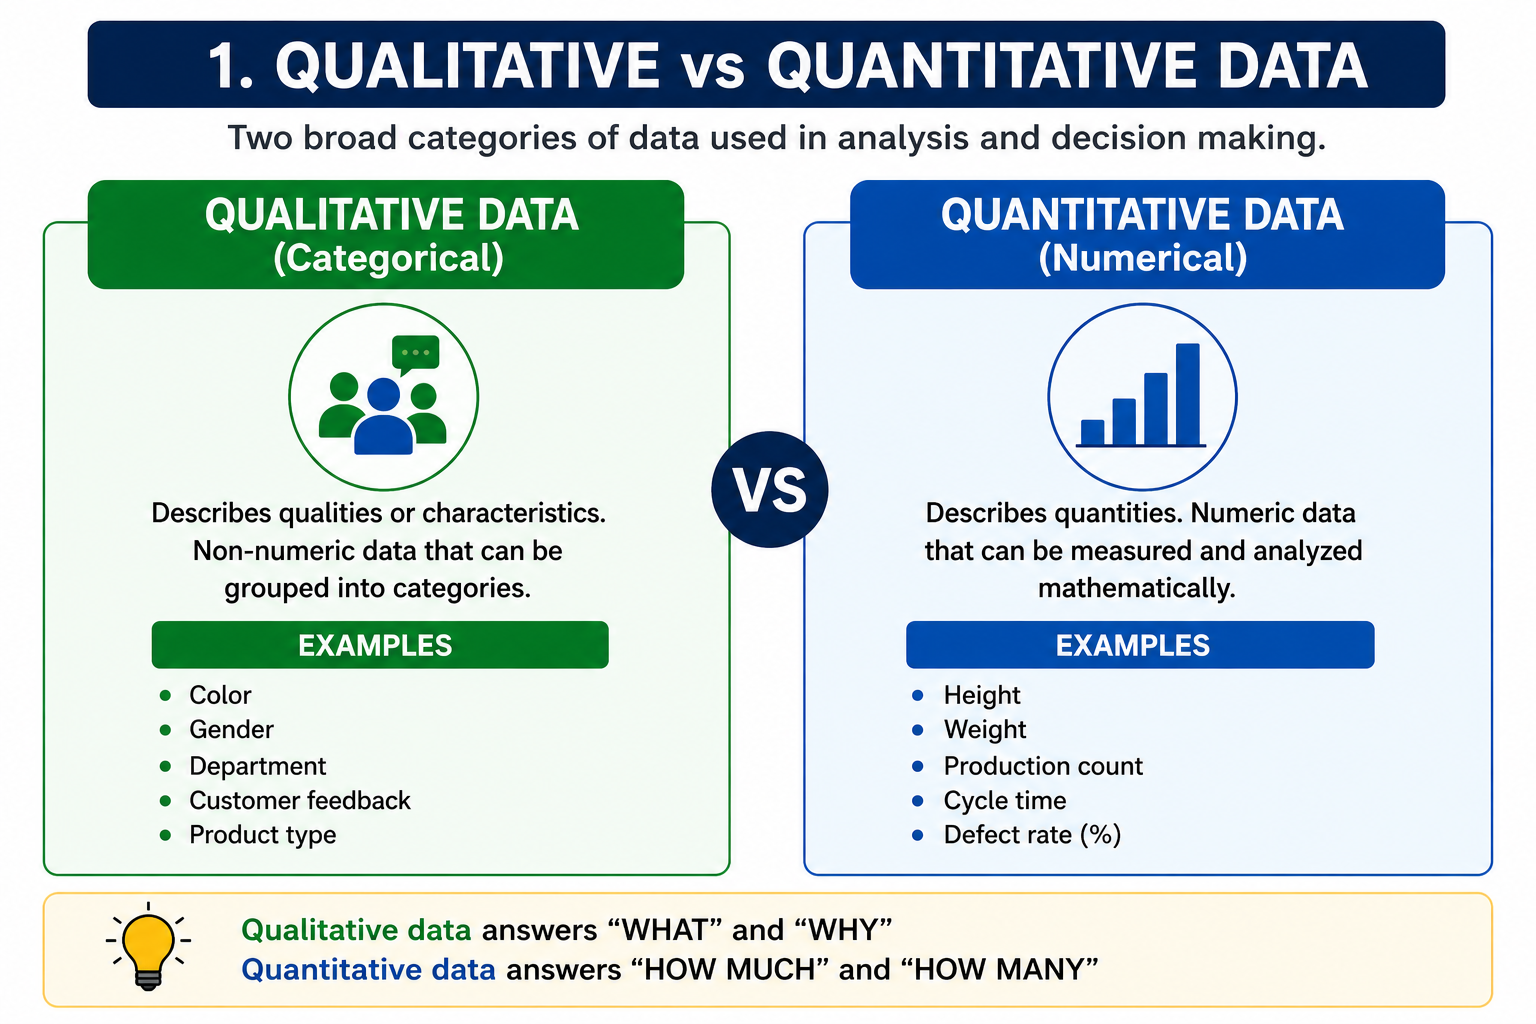
Why Many Six Sigma Projects Fail Before They Begin Most Six Sigma projects don’t fail because teams lack enthusiasm. They fail quietly, early, and invisibly—because the wrong data is collected, measured incorrectly, or analysed using the wrong method. Imagine spending weeks collecting data, only to realise later that: The data cannot be analysed statistically The charts chosen don’t fit the data type The conclusions are challenged by stakeholders The improvement actions are based on weak evidence This is not a tools problem. This is a data literacy problem. In Six Sigma, data is not just input. It is the foundation on which your Define, Measure, Analyze, Improve, and Control phases stand. If that foundation is weak, everything built on top of it becomes unstable. Understanding data types is what separates professional problem-solving from guesswork. When teams clearly know what kind of data they are working with, they choose the right charts, the right tests, and the right improvement actions—with confidence. What Do We Really Mean by “Data” in Six Sigma? In everyday work, we often say “I have data” when what we really have are scattered numbers, partial records, or subjective observations. In Six Sigma, data has a stricter meaning. Data is structured information collected using defined rules to describe how a process behaves. For example: The number of defective parts produced per shift The time taken to resolve a customer ticket The temperature of a machine at different intervals Customer satisfaction ratings after a service interaction Each of these represents a different type of data, and each requires a different method of analysis. Treating them all the same is one of the fastest ways to reach the wrong conclusion. This is why the first question a Six Sigma professional asks is not: “How much data do we have?” But: “What type of data are we dealing with?” Quantitative and Qualitative Data: Two Very Different Worlds At the highest level, Six Sigma data falls into two broad categories: quantitative and qualitative. The difference is more than academic—it determines what analysis is valid. Quantitative data is numerical. It represents measurable quantities such as time, weight, cost, length, or counts. When you measure cycle time in minutes, defect rate in percentages, or downtime in hours, you are working with quantitative data. This type of data allows deeper statistical analysis. You can calculate averages, variation, trends, correlations, and relationships. Most Six Sigma tools—histograms, control charts, regression—depend on quantitative data. Qualitative data, on the other hand, describes categories, attributes, or qualities. It answers questions like: What type of defect is this? Which department handled this request? Is the customer satisfied or not? Qualitative data is extremely valuable for understanding patterns, segmentation, and root cause themes, but it cannot be analysed using the same statistical methods as numerical data. Treating qualitative data like quantitative data—for example, averaging satisfaction categories—creates misleading insights. Strong Six Sigma projects use both. Qualitative data often helps frame the problem. Quantitative data helps prove the solution. Discrete and Continuous Data: Not All Numbers Behave the Same Even within quantitative data, not all numbers are equal. Some numbers are counted. Others are measured. This distinction affects everything from chart selection to hypothesis testing. Discrete data comes from counting. It represents whole numbers and cannot be subdivided meaningfully. You can count the number of defects, the number of calls received, or the number of errors in a report. You cannot have 2.6 defects in a unit—it is either defective or not. Continuous data comes from measurement. It can take any value within a range. Time taken to process an application can be 3.2 minutes, 3.27 minutes, or 3.271 minutes depending on measurement precision. Temperature, length, speed, and weight are all continuous. Why does this matter? Because Six Sigma tools assume certain data behaviours. Control charts for counts differ from control charts for measurements. A histogram of time behaves differently from a histogram of defect counts. Mixing these up leads to incorrect conclusions about stability and performance. Professionals who master this distinction can immediately spot when a team is using the wrong analysis method. Understanding Measurement Scales: Nominal, Ordinal, Interval, and Ratio Beyond data type, Six Sigma professionals also care about measurement scales. This determines what kind of mathematical operations and comparisons are valid. Nominal data is purely categorical. There is no inherent order. For example, product categories, defect types, or machine IDs. You can count frequency, but you cannot rank or average them. Ordinal data has a meaningful order but unequal spacing. Customer satisfaction ratings such as “Poor, Average, Good, Excellent” fall into this category. While “Excellent” is better than “Good,” the distance between these categories is not mathematically equal. This means that calculating averages can be misleading. Interval data has equal spacing between values, but no true zero. Temperature in Celsius is a classic example. The difference between 20°C and 30°C is the same as between 30°C and 40°C, but 0°C does not mean “no temperature.” This affects ratio-based interpretations. Ratio data has equal spacing and a true zero. Time, weight, cost, and distance fall here. This is the most powerful scale in Six Sigma because all statistical operations are valid. Understanding these scales prevents one of the most common analytical mistakes: performing mathematically valid calculations on data that does not support them conceptually. Why Data Type Directly Determines the Tool You Should Use In Six Sigma, tools are not chosen based on preference—they are chosen based on data type. When you use a histogram, you assume continuous data. When you use a p-chart, you assume binary outcomes. When you use regression, you assume numerical relationships. When you use a Pareto chart, you assume categorical frequency. When teams mismatch tools and data, they still get charts—but the charts tell the wrong story. Leaders may approve changes based on misleading analysis, and months later, the process slips back into old behaviour. Professionals who understand data types don’t just “use tools.” They choose tools strategically, ensuring every insight is defensible in front of stakeholders, auditors, and leadership. Real-World Example: How Wrong Data Types

Explore More

Subscribe to Our Newsletter

©2026, ICEQBS All Rights Reserved.